Completed & delivered to site

Q3 2024 Riyadh Rolling & Fabrication Complex

Mining, Gold Extraction & Heavy Chemical Industries

Leaching and filtration tanks for gold mines

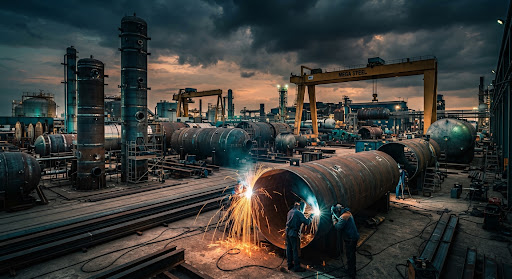
Leaching and filtration tanks fabricated for gold processing lines at mine sites.

Technical Documentation & Operations Gallery

4 high-resolution photos

Client Requirement & Operating Constraints

A major gold mine expansion needed four giant Carbon-In-Column (CIC) vessels, perfectly vertical and 3.2 m in diameter, to circulate gold slurry carrying abrasive cyanide compounds and acids under continuous operating pressure.

Strict defined criteria:

  • Zero mechanical or chemical corrosion defects over a design life of at least 25 years.
  • Mandatory compliance with the ASME Boiler and Pressure Vessel Code (Section VIII).
  • Certified hydrostatic testing witnessed by an internationally accredited third-party inspector (TPI).

Mega Steel Scope of Work (Execution Phases)

  1. Phase 01

    Engineering & Shop Drawings

    Structural calculations, 3D modelling in SolidWorks, and highly precise cutting and machining drawings.

  2. Phase 02

    Steel & Alloy Supply and Testing

    Certified carbon plates and resistant duplex alloys, PMI and ultrasonic tested to rule out laminations.

  3. Phase 03

    Rolling & Dished Ends

    Cold cylindrical rolling of 24 mm plate on CNC 4-roll machines, and code-compliant torispherical heads.

  4. Phase 04

    Assembly & Code Welding

    Automatic submerged arc (SAW) and gas tungsten arc (GTAW) welding to ASME-qualified WPS / PQR procedures.

Engineering Materials & Alloys Used

Certified, documented engineering

  • Treated carbon steel for pressure vessels
  • Two-phase duplex stainless steel alloy
  • Forged heavy flanges
  • High-strength alloy studs and bolts

ENGINEERING BOTTLENECKS

The Project’s Complex Engineering Challenges

  • Controlling Ovality & Thermal Distortion

    With a 3,200 mm diameter and 24 mm walls, repeated welding heat threatened to distort the shell beyond the ASME roundness tolerance of 0.5% of the nominal diameter.

  • Dissimilar Metal Welding

    Joining internal SS 2205 duplex parts to the A516 carbon steel shell without hydrogen cracking or brittle sigma phase weakening the weld’s corrosion resistance.

  • Nozzle Orientation

    More than 18 nozzles of different sizes and depths per vessel needed strict alignment to meet the site feed piping without installation stress.

ENGINEERED RESOLUTION

Innovative Engineering Solutions Applied

  • Internal Spider Jigs

    Radial hydraulic jigs held the shell during welding to prevent shrinkage, with a symmetric weld sequence that achieved 99.85% roundness.

  • Preheat Protocol with Inconel & High-Nickel Filler

    ERNiCrMo-3 (Inconel 625) filler for the dissimilar joints, interpass temperature kept below 150°C, and ferrite checked with a Ferritoscope for full metallurgical balance.

  • Horizontal CNC Machining with 3D Laser Inspection

    After welding, the shell was machined on a giant lathe so flange faces and nozzles sit within ±0.02 mm, verified with a laser tracker.

Custom Engineering Fabrication Solutions

Do you have a project that needs pressure vessels or specialised mechanical fabrication?

Send your materials list, engineering drawings or samples for immediate review by our engineers, who will define the best technical path and schedule.